Related Topics:
Flame Cabel Coating Fireproof-
Waterproof electrical distribution box coating
In order to improve the waterproof performance of industrial power distribution box, manufacturers will apply a layer of special waterproof coating on the surface of the box. This coating has good adhesion and weather resistance, and can effectively resist erosion by rainwater . (1) Waterproof distribution box engineered for harsh outdoor and industrial environments, providing IP65–IP68 sealing against dust, rain, and UV. Typically constructed from durable, corrosion-resistant materials, these boxes are designed to withstand exposure to moisture and harsh environmental. CE-TEK have developed over the last 30 years a comprehensive range of rugged Electrical Junction Boxes specifically for use in most Hazardous Areas within such industries as Oil & Gas, Petro-Chemical, Pharma, waste water, food and beverage, milling etc, indeed any application or location where the. Distribution boxes are a component of your electrical supply system dividing electrical power feeds into subsidiary circuits while offering a protective fuse or circuit breaker for every circuit in a common enclosure. To make sure these boxes work well, the right waterproof levels must be in place.
[PDF Version]
-
Requirements for electrical distribution boxes for coating equipment
Electrical requirements in a Powder Coating Booth include power supply, grounding systems, control panels, and safety-compliant wiring. Electrical and electronic enclosures are more than protective boxes—they safeguard people, ensure system reliability, and meet compliance. In modern industrial power distribution systems, surface coating is a common technical approach for the outer surface of components ss electrical enclosures. This process involves depositing metal or other functional materials onto the substrate surface to form a continuous coating. This section concentrates upon commonly used power distribution equipment: Panelboards, Switchboards, Low-Voltage Motor Control. Design requirements for low voltage distribution boxes cover NEC, IEC, and safety standards to ensure reliable, compliant electrical installations. Properly powder coated metal enclosures have very high resistance to peeling and cracking in addition to high chemical, corrosion and abrasion resistance.
[PDF Version]
-
Surface coating of distribution boxes
In order to improve the waterproof performance of industrial power distribution box, manufacturers will apply a layer of special waterproof coating on the surface of the box. This process involves depositing metal or other functional materials onto the substrate surface to form a continuous coating. the surface treatment specification includes the requirements of color. abinet must be optimally sealed in its overall construction. And the control cabinet standard DIN EN (IEC ) stipulates t at control cabinets must be equipped with a seamless. This paper introduces the process flow, color card selection and attention of metal distribution box customized color. Why do you need to customize colors? Brand recognition:Enterprises can spray the distribution boxes with the exclusive color consistent with the LOGO to enhance the on-site. Our powder-coated steel distribution box is designed to offer a rugged, reliable, and affordable solution for indoor electrical distribution systems.
[PDF Version]
-
Do all indoor cable trays need to be fireproof
Do all cable trays need fire resistance testing? Yes, especially for industrial, commercial, and high-risk areas. This includes checking their flammability, smoke production, toxic gas emissions, and ability to block heat and fire. Why Does. Where cables pass through shafts, walls, slabs, or enter electrical panels or cabinets, openings shall be tightly sealed with firestopping materials in accordance with design requirements. Process flow: reserved openings → busway installation → distribution box positioning and installation →. To uncover the answer to this question, we have conducted tests on cable tray systems in different materials. Through these tests the aim was to learn more about thermal conductivity properties in fire conditions and what effects it would have on the tray itself and how long the installed cable. Safety of a cable tray is not a matter of compliance with codes, but a matter of saving human life and billions of dollars' worth of infrastructure.
[PDF Version]
-
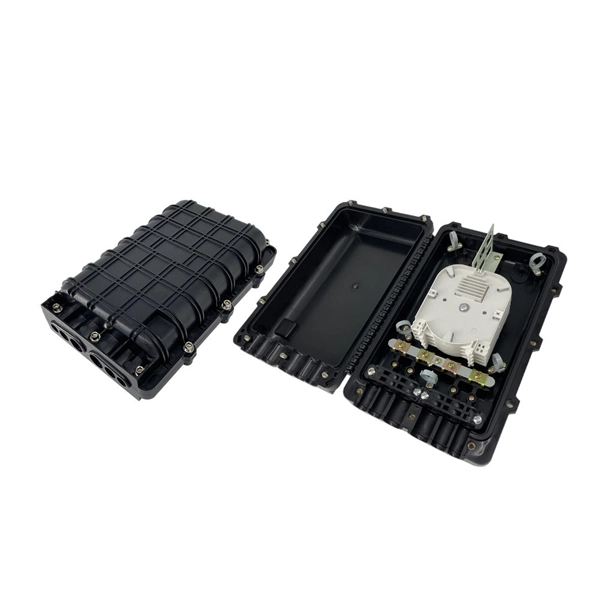
Fire resistance rating testing of fireproof cable trays
Fire resistance testing evaluates how well cable trays can withstand fire and prevent flames from spreading. This includes checking their flammability, smoke production, toxic gas emissions, and ability to block heat and fire. This is a test for electric cable systems that are required to maintain circuit integrity, so is therefore written around and is dependent on the cables themselves, but containmen of 90 minutes (the maximum time covered by DIN 4102-12). Understanding UL 1257 The UL 1257 testing standard evaluates the performance of cable tray and conduit. Cablofil cable tray is the preferred choice for the cable containment of low and high voltage electric cables where fire resistance is crucial - this includes cable basket tray systems for Prysmian FP (FP400 and FP600) and Draka Firetuf type cables.
[PDF Version]
-
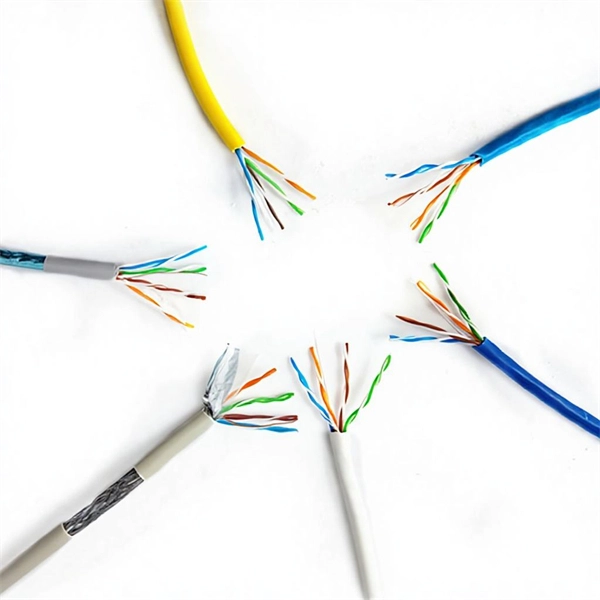
Introduction to Fireproof Fiberglass Cable Trays
FRP cable trays (fiberglass cable trays) are a new type of cable support device made primarily of glass fiber reinforced plastic, combined with flame retardants, stainless steel shielding mesh, and other materials. They are manufactured using a molding process, with core materials including glass. Effective protection of cable systems around the world: our tried-and-tested FLAMMOTECT-A and DG-CR 0. 7 products are successfully used to protect cables in high-rise buildings, industrial buildings, and offshore facilities as well as in sensitive areas, such as hospitals, airports, production. Fire resistance is a key factor when selecting cable trays for areas where fire hazards are present. These systems prevent fire and smoke from spreading through open cable pathways, maintaining circuit integrity and code. This document outlines the key requirements for cable tray layout, installation, and fireproofing in industrial and commercial environments.
[PDF Version]
-
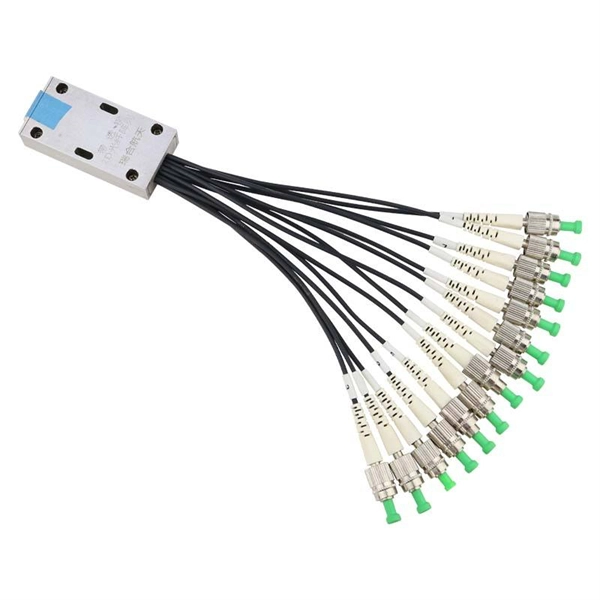
Which fireproof sleeve for optical cables is the best
OFNP (Plenum Rated): This is the highest fire rating, suitable for plenum areas (e., air ducts and ceiling voids). The BSTFLEX sleeve uses a silicone coated fiberglass construction to provide heat insulation for hoses, wires, and fuel lines. It withstands continuous operation temperatures from -60 C to 260 C and is VW-1 rated for flame resistance. Explore our expert reviews and secure your electrical setup today. High-amperage electrical systems in off-grid dwellings and mobile setups demand absolute reliability, where a single insulation failure can. Fire rated sleeves are essential protective coverings designed to shield hoses, cables, and wiring from extreme heat, flames, and molten splashes. Each product prioritizes heat resistance, ease of. When wiring, hoses, or fuel lines run near high-heat components, a reliable fire sleeve is essential.
[PDF Version]